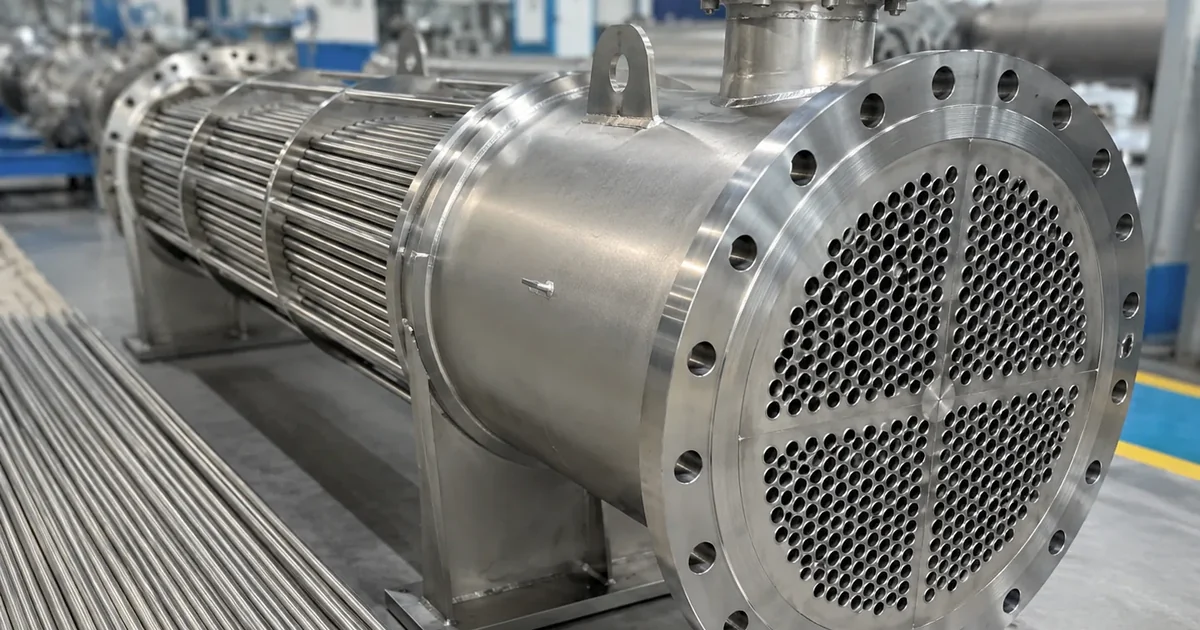
A titanium tube can have the correct grade on a quotation and still create installation or acceptance problems if the purchaser does not control material identity, dimensions, surface condition, tube integrity, test records and traceability. For ASTM B338 heat-exchanger and condenser tubing, inspection requirements also depend on whether the product is welded, seamless or welded/cold worked. A good purchase order therefore defines both the governing standard and the project-specific inspection package before production begins.
ASTM B338 inspection requirements: construction route matters
ASTM B338 covers titanium and titanium-alloy tubing intended for surface condensers, evaporators and heat exchangers. The current ASTM listing is B338-17(2026). Its published abstract distinguishes testing by tube construction.
| Tube construction | Published ASTM B338 inspection basis | Buyer action |
|---|---|---|
| Welded tubing | Nondestructive electromagnetic testing plus ultrasonic testing; hydrostatic or pneumatic testing | State the purchased edition and require corresponding reports when documentation is needed |
| Seamless tubing | Ultrasonic testing; electromagnetic or hydrostatic or pneumatic testing as permitted by the standard | Confirm the selected route and required report package |
| Welded / cold-worked tubing | Ultrasonic testing is identified in the current ASTM abstract | Define construction clearly so the correct acceptance basis is used |
This overview does not replace the full purchased standard. The exact edition stated in the contract controls detailed acceptance criteria, sampling and supplementary requirements.
For specification planning before inspection, see ASTM B338 Titanium Tube RFQ Guide.
1. Verify titanium grade, standard and construction
Start with the purchase-order identity rather than surface appearance. Confirm the material grade, UNS designation where applicable, ASTM B338 or ASME SB-338 basis, purchased edition, seamless/welded/welded-cold-worked construction, heat or lot number and PO line item.
2. Review the MTC / MTR before release
The material certificate should be checked against the purchase order, not merely collected as a PDF. Typical review points include grade, standard, heat or lot identity, chemistry, mechanical properties, ordered condition and any agreed test references.
Material identity
Grade, standard, heat/lot number and product description should agree with the PO.
Chemical composition
Review reported chemistry against the applicable grade requirements.
Mechanical properties
Check required tensile and other mechanical results against the ordered standard.
Test references
If reports are required, ensure NDT or pressure-test records are traceable to the lot.
Traceability
MTC, bundle marking, packing list and inspection records should use a consistent identity chain.
Certificate type
If EN 10204 3.1, 3.2 or another format is required, define it before quotation.
3. Dimensional inspection: OD, wall thickness and finished length
Heat exchanger tubes are assembly components. Dimensional errors can affect tube-sheet fit-up, rolling, welding, bundle installation and final tube count. The inspection plan should identify OD, wall thickness, finished length, applicable tolerances, ovality if controlled, straightness where project-specific and tube-end condition.
4. Wall-thickness inspection for thin-wall tubes
Many condenser and exchanger projects use thin-wall titanium tubing. As wall thickness decreases, measurement method and tolerance control become more important. If minimum wall at any point is critical, write that requirement clearly rather than relying on nominal wall alone.
5. Visual inspection: define what acceptable means
A useful visual inspection checks for cracks, folds, dents, deep scratches, handling damage, tube-end damage, oxidation, contamination, dirt, oil, marking legibility and packing damage. Acceptance should follow the standard and project specification, not subjective descriptions such as “premium surface.”
6. Eddy current / electromagnetic testing
The current ASTM B338 abstract states that welded tubing is tested using a nondestructive electromagnetic method in addition to ultrasonic testing. For seamless tubing, the abstract lists an electromagnetic or hydrostatic or pneumatic route in addition to ultrasonic testing.
Before placing the order, define the applicable test method, reference standard, coverage, calibration/reference standard, acceptance criteria, report requirement and any TPI witness point.
7. Ultrasonic testing
The current ASTM B338 abstract identifies ultrasonic testing for welded tubing and for seamless and welded/cold-worked tubing. Avoid writing only “100% UT” without an acceptance basis. The PO or ITP should identify the applicable method, coverage, calibration basis and reporting requirement.
8. Hydrostatic or pneumatic testing
Pressure or leak testing verifies a different aspect of tube integrity from UT or electromagnetic inspection. The current ASTM B338 abstract states that welded tubing is tested with a hydrostatic or pneumatic method, while seamless tubing includes electromagnetic or hydrostatic or pneumatic routes in addition to the applicable UT requirement.
Confirm the selected method, pressure basis, hold requirement if applicable, acceptance criterion, recording requirement and cleaning/drying requirement after hydrostatic testing.
Do not use “1.5× design pressure” as a universal titanium tube requirement unless the governing standard, code or purchaser specification actually calls for it.
9. Flattening and reverse-flattening tests
ASTM B338 includes forming-related mechanical tests. The current ASTM abstract notes flattening requirements for tubing and a reverse-flattening test for welded tube. Buyers should verify that required test results are represented in the manufacturing and certification package according to the purchased standard.
10. Surface condition and cleanliness
For heat exchanger applications, surface condition can affect expansion, welding, cleaning and incoming inspection. State requirements for pickled or cleaned surface, internal cleanliness, degreasing, roughness if project-specific, tube-end protection and protection from carbon-steel contamination.
11. PMI: useful, but not a substitute for certification
PMI can be useful for multi-alloy projects, first orders or critical applications. If required, define the sampling scope, instrument/method where controlled, identification criteria, report format and TPI involvement. For commercially pure titanium grades, understand the limitations of the selected PMI technology before using it as the sole grade-verification method.
12. Heat-number and lot traceability
If this chain breaks, a buyer may have technically good tubes but insufficient evidence to release them into an EPC or regulated project.
13. When should buyers use third-party inspection?
TPI is not necessary for every order. It becomes more useful for first orders with a new supplier, large condenser quantities, EPC or owner-mandated projects, fixed-length tubes, critical NDT witness points, complex documentation packages or pre-shipment packing release.
14. Build the ITP before production
| Stage | Typical inspection item | Possible purchaser status |
|---|---|---|
| Raw material | Material identity / certificate review | Review |
| Production | Dimensions / process controls | Surveillance or record review |
| NDT | ECT / electromagnetic / UT as applicable | Witness or review |
| Pressure / leak test | Hydrostatic or pneumatic where applicable | Witness or report review |
| Final inspection | Dimensions, surface, marking, quantity | Witness / hold point if specified |
| Documentation | MTC, NDT, dimensional and release records | Hold until approved if contractually required |
| Packing | Protection, bundle marking, packing list | Final release |
15. Pre-shipment packing inspection
Long thin-wall titanium tubes can pass production inspection and still be damaged during export handling. Before shipment, verify tube count, bundle identification, heat/lot marking, end protection, cleanliness, crate or bundle condition, waterproofing if specified, lifting arrangement, packing-list consistency and shipping marks.
16. Final document package
Depending on the PO, buyers may require the commercial invoice, packing list, MTC/MTR, chemistry and mechanical results, NDT reports, pressure-test report, dimensional report, final inspection record, PMI report if ordered, TPI release note and project-specific shipping documents.
ASTM B338 pre-shipment inspection checklist
| Check | Buyer question |
|---|---|
| Grade | Does the tube and MTC match the ordered titanium grade? |
| Standard | Is the correct ASTM/ASME standard and edition stated? |
| Construction | Is seamless / welded / welded-cold-worked construction correct? |
| Dimensions | Are OD, wall, length and project tolerances verified? |
| Surface | Are visible defects, cleanliness and tube ends acceptable? |
| UT | Has required ultrasonic testing been completed and documented? |
| ECT / electromagnetic | Has applicable electromagnetic inspection been completed? |
| Pressure test | Has the required hydrostatic or pneumatic route been completed? |
| Mechanical tests | Are required tensile / flattening / reverse-flattening results documented? |
| Traceability | Do heat/lot numbers connect tubes, reports, MTC and packing? |
| TPI | Are witness / hold points signed off if TPI was ordered? |
| Packing | Are quantity, marking, protection and export packing correct? |
Example RFQ inspection wording
ASTM B338 Grade 2 titanium heat exchanger tubes · OD ___ mm × WT ___ mm × L ___ mm · ___ pcs · construction ___ · dimensional inspection per PO and drawing · applicable ASTM B338 NDT and pressure testing · MTC with heat/lot traceability · final visual and dimensional report · third-party inspection option to be quoted separately · export packing for long tubes.
Common inspection mistakes
- requesting “100% inspection” without identifying the methods;
- using different ASTM editions in the PO and ITP;
- forgetting to state seamless or welded construction;
- accepting an MTC without checking heat-number traceability;
- adding hold points after production is complete;
- copying arbitrary ECT or UT limits from another supplier;
- checking OD and length but not wall thickness;
- ignoring tube-end and packing damage;
- treating PMI as a replacement for material certification;
- not defining the document package before shipment.
Related titanium tube procurement guides
Titanium Tube Supplier & Product Hub →
- Titanium Heat Exchanger Tube
- Titanium Heat Exchanger Tubes Buyer Guide
- ASTM B338 Titanium Tube RFQ Guide
- How to Specify a Titanium Tube RFQ
- Titanium Tube Supplier Selection Guide
- Titanium Seamless vs Welded Tube
- Grade 2 Titanium Tube for Heat Exchangers
Frequently asked questions
What inspections are required by ASTM B338?
Requirements include material, mechanical and tube-integrity controls, with NDT and pressure-test routes depending on tube construction. Always use the exact purchased edition.
Does welded B338 tubing require ECT?
The current ASTM B338 abstract states that welded tubing is tested using a nondestructive electromagnetic method as well as ultrasonic testing.
Does B338 require UT?
The current ASTM abstract identifies UT for welded tubing and for seamless and welded/cold-worked tubing.
Should I request an MTC?
Industrial buyers commonly require an MTC or MTR to support grade, chemistry, mechanical properties and traceability.
Do I need third-party inspection?
Not for every order. It is most useful for critical projects, first orders, large quantities or owner/EPC requirements.
Reference source
Primary standard reference: ASTM B338-17(2026) — Standard Specification for Seamless and Welded Titanium and Titanium Alloy Tubes for Condensers and Heat Exchangers. The full purchased standard and project documents remain controlling for inspection and acceptance.
Request a quote for ASTM B338 titanium tubes
Send grade, construction, OD × wall × length, quantity, standard edition, NDT, pressure-test, MTC, TPI and packing requirements. If you have an ITP or purchaser specification, attach it with the RFQ.
 Scan to chat on WhatsApp